Metal stamping is one of the most widely used manufacturing processes for producing precision metal components in industries such as automotive, electronics, aerospace, construction, and industrial equipment. By applying controlled pressure through specialized dies and presses, manufacturers can transform flat metal sheets into components with specific shapes, dimensions, and functional features.
For businesses sourcing metal components, understanding how metal stamping works is essential to selecting the right manufacturing process, controlling production costs, and ensuring consistent product quality.
Metal stamping is a manufacturing process that uses a stamping press and custom-designed dies to cut, bend, form, or shape sheet metal into specific components.
During production, a metal sheet or coil is positioned between two sections of a die. The press applies mechanical or hydraulic force, causing the material to take the required shape. Depending on the die design and production requirements, multiple operations can be completed in a single press cycle.
Metal stamping is particularly suitable for producing large quantities of identical components with consistent dimensions and repeatable quality.
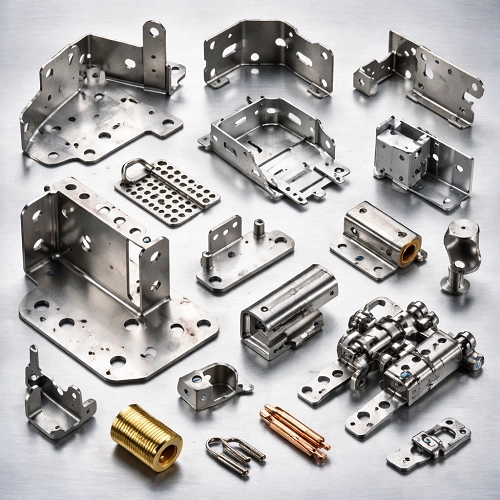
Common stamped products include:
Automotive brackets and structural components
Electrical connectors and terminal components
Metal enclosures and housing parts
Industrial mounting plates and clips
Appliance components
Precision metal springs and retaining clips
Unlike machining, which removes material to create a finished shape, stamping primarily uses forming and cutting operations to process sheet metal. This makes it an efficient solution for many high-volume manufacturing applications.
Metal stamping involves several interconnected stages. Each stage contributes to the dimensional accuracy, surface quality, and overall performance of the finished component.
The manufacturing process begins with selecting a suitable metal material based on the component's functional requirements.
Important considerations include material thickness, tensile strength, ductility, corrosion resistance, and formability.
For example, stainless steel may be selected for components requiring corrosion resistance, while aluminum is often used when lightweight construction is important.
The stamping die determines the geometry and accuracy of the finished component.
Engineers develop the die according to the product drawing, material specifications, thickness, tolerances, and production volume.
Depending on the component's complexity, the tooling may incorporate multiple stations to perform different operations in sequence.
Proper die design is essential because tooling errors can lead to dimensional inconsistencies, excessive material waste, burr formation, or premature tool wear.
The selected metal sheet or coil is fed into the stamping press. The press applies controlled force through the die to perform the required operations.
These operations may include cutting, punching, bending, drawing, or forming.
After the main stamping operation, some components require additional processing to meet their functional or appearance requirements.
Common secondary operations include:
Deburring and edge finishing
Thread tapping and hole finishing
Welding and assembly
Surface polishing
Plating and coating
Heat treatment
Not every stamped component requires all these processes. The finishing requirements depend on the product's design and intended application.
Finished components are inspected against the approved engineering specifications.
Typical inspection items include dimensional accuracy, hole position, material thickness, surface condition, burr height, and forming consistency.
For critical components, manufacturers may also use specialized measuring equipment and functional testing to verify product performance.
Different stamping techniques are used depending on component geometry, material characteristics, production volume, and dimensional requirements.
Progressive die stamping is a high-efficiency process in which a metal strip moves through multiple stations within a single die.
Each station performs a specific operation, such as punching, bending, or forming. As the material advances through the die, the component gradually takes its final shape.
Key advantages:
High production efficiency
Consistent part quality
Suitable for complex geometries
Reduced manual handling
Effective for high-volume manufacturing
Progressive stamping is commonly used for automotive components, electrical terminals, precision clips, and electronic hardware.
Transfer stamping uses a system that moves individual metal blanks between multiple processing stations.
Unlike progressive stamping, where the component remains connected to the metal strip during processing, transfer stamping separates the blank before moving it through subsequent operations.
Key advantages:
Suitable for larger or deeper components
Supports complex forming operations
Allows independent processing at different stations
Provides flexibility for certain component geometries
This process is frequently used for automotive structural parts, deep-drawn components, and larger industrial metal products.
Deep drawing is a forming process used to manufacture hollow or cup-shaped metal components from flat sheet material.
A punch pushes the sheet into a die cavity, causing the material to flow and form the required shape without intentionally cutting away the main body of the material.
Typical applications include metal containers, automotive housings, appliance components, and cylindrical enclosures.
The success of deep drawing depends on material ductility, blank-holder force, die geometry, lubrication, and drawing depth.
Poor process control can result in wrinkling, tearing, thinning, or uneven wall thickness.
Blanking and punching are cutting operations used to produce specific shapes or openings in sheet metal.
Although they use similar tooling principles, their purposes are different:
Blanking: The cut-out piece is the desired finished component.
Punching: The hole created in the sheet is the required feature, while the removed material is scrap.
These operations are widely used for mounting plates, washers, electrical components, brackets, and metal panels.
Bending changes the angle or shape of a metal sheet without intentionally separating the material.
Common bending operations include V-bending, U-bending, edge bending, and offset bending.
Manufacturers must consider springback, which occurs when metal partially returns toward its original shape after the forming force is removed.
Accurate tooling compensation and appropriate process parameters help achieve the required final angles and dimensions.
Material selection directly affects production efficiency, tooling life, component performance, and manufacturing costs.
The following materials are commonly used in sheet metal stamping.
| Material | Main Characteristics | Typical Applications |
|---|---|---|
| Carbon Steel | Good strength, formability, and cost efficiency | Brackets, automotive parts, structural components |
| Stainless Steel | Corrosion resistance and mechanical strength | Medical equipment parts, appliances, industrial components |
| Aluminum | Lightweight, corrosion resistant, and formable | Automotive parts, electronic housings, panels |
| Copper | Excellent electrical and thermal conductivity | Electrical connectors, terminals, conductive components |
| Brass | Good conductivity, machinability, and corrosion resistance | Electrical fittings, precision hardware |
| Galvanized Steel | Zinc-coated surface provides corrosion protection | Enclosures, brackets, construction hardware |
The best material depends on the operating environment and functional requirements of the component.
For example:
Choose stainless steel when corrosion resistance and durability are important.
Consider aluminum when weight reduction is a priority.
Use copper for components requiring high electrical conductivity.
Select carbon steel for cost-effective structural and mechanical applications.
Material thickness must also be evaluated carefully. Thicker materials generally require greater stamping force and may increase tooling demands, while thinner materials can be more susceptible to wrinkling, distortion, and handling damage.
Achieving consistent stamped components requires more than selecting an appropriate press. Material properties, tooling design, process parameters, and inspection methods all influence the final result.
Differences in material thickness, hardness, tensile strength, and ductility can affect how metal behaves during stamping.
Even materials with the same nominal specification may exhibit variations between production batches. These differences should be considered when establishing process parameters.
The stamping die directly influences dimensional accuracy, cutting quality, and production stability.
Poor die clearance can create excessive burrs, while worn cutting edges may cause inconsistent dimensions and poor surface conditions.
Regular die inspection, cleaning, sharpening, and preventive maintenance help maintain production consistency.
The stamping press must provide sufficient force and appropriate operating characteristics for the selected material and component geometry.
Important parameters include:
Press tonnage
Stroke length
Operating speed
Die shut height
Feed accuracy
Material positioning
Incorrect settings may lead to incomplete forming, dimensional deviations, material cracking, or tooling damage.
Lubrication reduces friction between the material and tooling during forming operations.
Appropriate lubricants can improve material flow, reduce surface scratching, and extend die service life.
The lubricant must be compatible with the material and subsequent manufacturing processes, especially when components require painting, plating, welding, or assembly.
A reliable inspection system should cover both initial production approval and ongoing manufacturing.
Useful quality control methods include:
First Article Inspection (FAI)
Coordinate Measuring Machine (CMM) inspection
Go/no-go gauge testing
Optical measurement
Surface defect inspection
Statistical Process Control (SPC)
For high-volume production, monitoring critical dimensions throughout manufacturing helps identify process deviations before they affect large quantities of parts.
Metal stamping offers several manufacturing advantages that make it an attractive option for industrial component production.
High Production Efficiency
Automated stamping presses can produce large quantities of components within relatively short production cycles. Progressive die stamping is particularly effective for continuous, high-volume production.
Consistent Product Quality
Once the tooling and process parameters are properly established, stamping can deliver repeatable component dimensions and geometries.
Cost Efficiency for Large Production Runs
Although custom tooling requires an initial investment, the cost per component can become competitive as production volume increases.
Material Utilization
Well-designed stamping layouts can optimize material usage and reduce scrap. Nesting and strip-layout optimization are important considerations when controlling raw material costs.
Design Flexibility
Metal stamping supports a wide range of shapes, holes, bends, embossing features, and formed geometries, allowing manufacturers to produce components for different industrial applications.
Understanding common stamping defects helps manufacturers improve production stability and reduce unnecessary costs.
| Common Defect | Possible Cause | Prevention Method |
|---|---|---|
| Burrs | Incorrect die clearance or worn cutting edges | Optimize clearance and maintain tooling |
| Cracking | Insufficient material ductility or excessive deformation | Review material selection and forming design |
| Wrinkling | Improper blank-holder force or material flow | Adjust forming conditions and die design |
| Springback | Material elastic recovery after bending | Compensate die geometry and control forming parameters |
| Surface Scratches | Poor lubrication or contaminated tooling | Improve lubrication and die cleanliness |
| Dimensional Variation | Material inconsistency, tool wear, or feeding errors | Monitor critical dimensions and maintain equipment |
Defect prevention should begin during product and tooling development rather than relying exclusively on final inspection.
For example, a component with a tight bending radius may require a different material grade or a redesigned forming sequence to avoid cracking.
Early engineering review can prevent expensive tooling modifications after mass production has started.
Metal stamping supports manufacturing requirements across a wide range of industries.
Automotive manufacturers use stamped metal components in both structural and functional assemblies.
Typical products include:
Mounting brackets
Seat components
Reinforcement panels
Electrical connectors
Battery-related metal components
Engine and transmission brackets
Automotive stamping often requires strict dimensional control, traceability, and repeatable production quality.
Metal stamping is widely used to produce small, precise components for electronic and electrical systems.
Examples include:
Electrical terminals
Contact springs
Connector housings
Shielding components
Conductive metal clips
Copper, brass, stainless steel, and specialized alloys are commonly selected according to conductivity, strength, and corrosion requirements.
Aerospace applications may require lightweight materials, precise geometries, and stringent material traceability.
Stamped components can be found in brackets, clips, equipment housings, and various supporting structures.
Material certification and documented inspection procedures are particularly important in this industry.
Stamped metal components are used in machinery, industrial enclosures, mounting systems, hinges, fastening hardware, and equipment supports.
Carbon steel, stainless steel, and galvanized steel are common choices depending on load requirements and environmental exposure.
Metal stamping is also essential in producing appliance panels, internal supports, mounting brackets, motor components, and structural housings.
Consistent dimensions and surface quality help ensure proper assembly and product appearance.
Metal stamping is not always the most suitable manufacturing solution. Comparing it with alternative processes helps determine the right approach for each component.
| Manufacturing Process | Main Advantages | Suitable Applications |
|---|---|---|
| Metal Stamping | High production speed and repeatability | High-volume sheet metal components |
| CNC Machining | High precision and flexible geometry | Complex parts and low-to-medium production volumes |
| Laser Cutting | Flexible cutting with minimal tooling requirements | Prototypes and sheet metal profiles |
| Metal Casting | Suitable for complex three-dimensional shapes | Housings and larger solid components |
| Metal Forging | Excellent mechanical properties for suitable geometries | High-strength load-bearing components |
For example, laser cutting may be more economical when producing a small number of flat metal prototypes because custom stamping dies are not required.
However, when production volumes increase and the design is stable, stamping may provide a lower unit cost and faster production cycle.
Some products also combine multiple processes. A stamped component may undergo CNC machining, welding, or surface finishing to achieve its final specifications.
Selecting the right manufacturing partner is important for maintaining product quality, delivery schedules, and long-term production costs.
Rather than comparing suppliers based only on unit prices, buyers should evaluate their technical capabilities and quality management systems.
Ask whether the manufacturer has the appropriate stamping equipment, press capacity, tooling capabilities, and automation systems for your product.
The supplier should be able to explain how its equipment supports your required material thickness, component dimensions, and production volume.
A capable manufacturer should understand die design, material behavior, forming limitations, and production optimization.
Ask whether engineering support is available for design reviews, manufacturability assessments, and tooling development.
Request information about quality inspection equipment, material traceability, production documentation, and nonconformance management.
For automotive applications, for example, IATF 16949 certification may be relevant. For other industries, ISO 9001 certification can provide useful evidence of an established quality management system.
However, certification alone does not guarantee product quality. Buyers should also evaluate actual inspection practices and production records.
Confirm whether the supplier can support your expected monthly demand and future volume increases.
Discuss tooling development time, sample approval, production lead times, and contingency arrangements.
A competitive quotation should clearly identify the major cost components, including:
Raw material costs
Tooling and die development
Stamping and processing fees
Secondary operations
Surface treatments
Packaging and transportation
A supplier offering a lower unit price may not necessarily provide the lowest overall production cost if tooling, scrap rates, quality issues, or delivery delays are not considered.
Providing complete technical information helps manufacturers evaluate feasibility and prepare more accurate quotations.
Before contacting a supplier, prepare the following:
Product drawings: Provide 2D engineering drawings and 3D CAD files when available.
Material specifications: Identify the required metal grade, material standard, and thickness.
Dimensional tolerances: Highlight critical dimensions, hole positions, flatness, and geometric requirements.
Surface requirements: Specify plating, coating, polishing, or other finishing treatments.
Production quantity: Provide estimated prototype, initial order, and annual production volumes.
Quality requirements: Identify inspection standards, material certification, and testing requirements.
Application details: Explain how the component will be installed and what mechanical or environmental conditions it must withstand.
One important recommendation is to distinguish between critical and non-critical dimensions.
Not every dimension requires an extremely tight tolerance. Applying unnecessarily strict tolerances can increase tooling complexity, inspection requirements, and manufacturing costs without improving the component's actual performance.
A clear drawing with functional tolerances helps the manufacturer balance quality and production efficiency.
Metal stamping continues to evolve as manufacturers adopt more advanced production technologies.
Automation is improving material feeding, part transfer, inspection, and production monitoring. These developments help reduce manual handling, improve process consistency, and increase manufacturing efficiency.
Several trends are particularly important:
Automated Production Lines: Robotic handling and automatic feeding systems support continuous production and reduce dependence on manual operations.
Advanced Die Design: CAD, simulation, and forming analysis tools help engineers identify potential forming problems before manufacturing physical tooling.
In-Line Quality Inspection: Optical inspection and automated measurement systems can detect dimensional deviations and surface defects during production.
Lightweight Material Processing: Growing demand for lightweight automotive and industrial components is encouraging manufacturers to develop stamping solutions for aluminum and advanced high-strength steels.
Sustainable Manufacturing: Material utilization, scrap recycling, energy efficiency, and longer tooling life are becoming increasingly important in manufacturing cost and environmental management.
These developments are making metal stamping more adaptable to modern production requirements, particularly where manufacturers must balance precision, production volume, and cost efficiency.